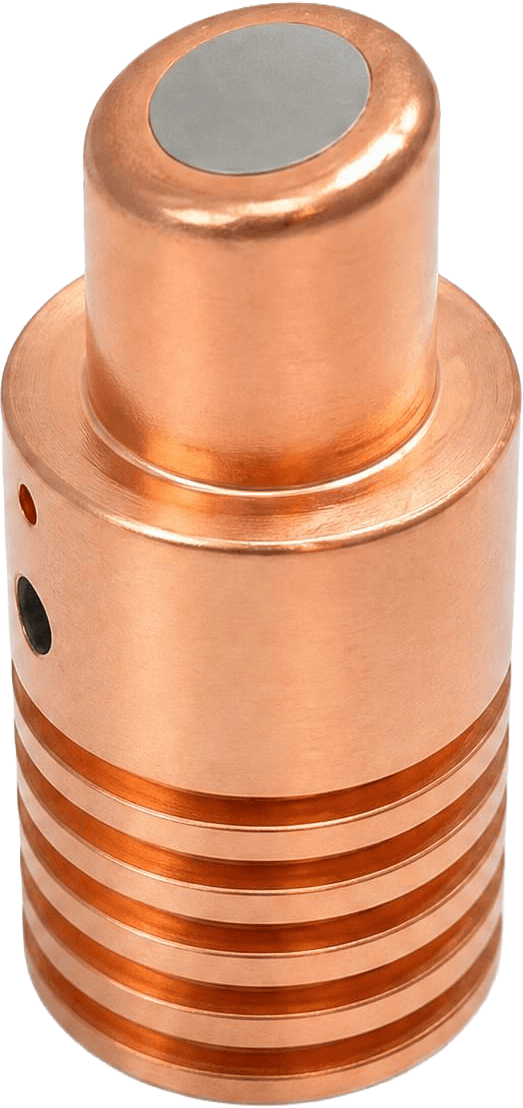
Cathode & Anode
Cathode & Anode
Cathode & Anode
Tungsten and molybdenum boats and crucibles for vacuum deposition and high-temperature melting. They are used where the vessel must not react with molten metal, and are built to your required shape and capacity.
Tungsten and molybdenum boats and crucibles for vacuum deposition and high-temperature melting. They are used where the vessel must not react with molten metal, and are built to your required shape and capacity.
Tungsten and molybdenum boats and crucibles for vacuum deposition and high-temperature melting. They are used where the vessel must not react with molten metal, and are built to your required shape and capacity.
Applied parts
Applied parts
Used as the evaporation source in vacuum coaters, the melting crucible in high-temperature furnaces and the vessel in crystal growth equipment. Material and shape are designed around what it will hold and at what temperature.
Used as the evaporation source in vacuum coaters, the melting crucible in high-temperature furnaces and the vessel in crystal growth equipment. Material and shape are designed around what it will hold and at what temperature.
Geometry, bonding and surface grade are set by the tube specification. Tell us the drawing and the service conditions and we will confirm and reply.
Geometry, bonding and surface grade are set by the tube specification. Tell us the drawing and the service conditions and we will confirm and reply.
KEY FEATURES
Density and atomic number set the shielding
The heavier and the higher the atomic number, the better it blocks radiation.

Density 19.3 g/cm³, atomic number 74. It blocks in a thinner section than lead at the same thickness.
High density
High Density
Far heavier than lead, it gives the same shielding performance in a thinner section.
Electron beam heat resistance
Beam Load
It withstands the heat at the focal spot where the electron beam lands and holds its shape.
Surface accuracy
Surface Finish
The roughness of the focal track governs X-ray output and service life.
Density by material
Density g/cm³. The higher the figure, the better the shielding at the same thickness.
Why it can be made thin
Its high density gives the same shielding in a thinner section. The equipment can be designed smaller.
Focal track control
As the focal track roughens, output falls. The surface grade is set alongside.
KEY FEATURES
Density and atomic number set the shielding
The heavier and the higher the atomic number, the better it blocks radiation.
Density by material
Density g/cm³. The higher the figure, the better the shielding at the same thickness.
Density 19.3 g/cm³, atomic number 74. It blocks in a thinner section than lead at the same thickness.
Far heavier than lead, it gives the same shielding performance in a thinner section.
Density 19.3 g/cm³, atomic number 74. It blocks in a thinner section than lead at the same thickness.
High density
High Density
Far heavier than lead, it gives the same shielding performance in a thinner section.
Electron beam heat resistance
Beam Load
It withstands the heat at the focal spot where the electron beam lands and holds its shape.
Surface accuracy
Surface Finish
The roughness of the focal track governs X-ray output and service life.
Density by material
Density g/cm³. The higher the figure, the better the shielding at the same thickness.
Why it can be made thin
Its high density gives the same shielding in a thinner section. The equipment can be designed smaller.
Focal track control
As the focal track roughens, output falls. The surface grade is set alongside.
DESIGN PRECISION
Geometry set to the tube
In a target, geometry and surface are what distinguish the product.

In the same target, changing the focal angle and the surface changes the output and the service life.
Machined geometry
Focal angle and track diameter are machined as drawn.
Surface condition
The focal face roughness is finished to specification.
Substrate joining
Where required, it is bonded to a molybdenum or graphite substrate.
We do not pick a specification, we develop it with you. (Give us the tube specification and the output conditions, and we will work out the geometry with you.)
DESIGN PRECISION
Geometry set to the tube
In a target, geometry and surface are what distinguish the product.
In the same target, changing the focal angle and the surface changes the output and the service life.
Machined geometry
Focal angle and track diameter are machined as drawn.
Surface condition
The focal face roughness is finished to specification.
Substrate joining
Where required, it is bonded to a molybdenum or graphite substrate.
We do not pick a specification, we develop it with you. (Give us the tube specification and the output conditions, and we will work out the geometry with you.)
APPLICATIONS
Applications
The fields where shielding parts and targets are used. Geometry differs by equipment.
APPLICATIONS
Applications
The fields where shielding parts and targets are used. Geometry differs by equipment.
LEAD TIME
Fabrication and Lead Time
This product is made to your drawing. Here is the process, step by step.
STEP 01
Drawing received
Send us the electrode dimensions, tip material, bonding method and cooling conditions.
Reply within 1 daySTEP 02
Specification review
We propose the copper body and tip combination and review the bonding conditions.
2 – 4 daysSTEP 03
Bonding · machining
The tip is bonded, then machined to the dimensions on the drawing and the heat dissipation section finished.
By agreement, depending on the production scheduleSTEP 04
Inspection · delivery
The joint and dimensions are verified, and the part ships with a test report. Repeat orders to the same drawing skip the review stage.
By agreement, depending on the production scheduleMinimum quantity
From 1 piece
Varies with geometry and bonding conditions.
Standard lead time
About 3 – 4 weeks
From drawing approval. Additional bond inspection items add to the period.
Supplied with it
Test report
Dimensional and joint inspection results are sent with the delivery.
LEAD TIME
Fabrication and Lead Time
This product is made to your drawing. Here is the process, step by step.
Drawing received
Send us the electrode dimensions, tip material, bonding method and cooling conditions.
From 1 piece
Varies with geometry and bonding conditions.
About 3 – 4 weeks
From drawing approval. Additional bond inspection items add to the period.
Test report
Dimensional and joint inspection results are sent with the delivery.
STEP 01
Drawing received
Send us the electrode dimensions, tip material, bonding method and cooling conditions.
Reply within 1 daySTEP 02
Specification review
We propose the copper body and tip combination and review the bonding conditions.
2 – 4 daysSTEP 03
Bonding · machining
The tip is bonded, then machined to the dimensions on the drawing and the heat dissipation section finished.
By agreement, depending on the production scheduleSTEP 04
Inspection · delivery
The joint and dimensions are verified, and the part ships with a test report. Repeat orders to the same drawing skip the review stage.
By agreement, depending on the production scheduleMinimum quantity
From 1 piece
Varies with geometry and bonding conditions.
Standard lead time
About 3 – 4 weeks
From drawing approval. Additional bond inspection items add to the period.
Supplied with it
Test report
Dimensional and joint inspection results are sent with the delivery.
HANDLING
Handling precautions
These apply to refractory metals in general. Service life depends heavily on how the parts are handled.
01
01
Do not touch the parts with bare hands after unpacking. Oil from fingerprints carbonizes at high temperature and becomes a contaminant.
02
02
The material is weak against impact and bending. Tungsten is brittle at room temperature and can crack if dropped.
03
03
Do not heat above 500°C in air; oxidation accelerates sharply. Always use the parts in a vacuum or an inert atmosphere.
04
04
Avoid rapid heating and cooling. On first use, we recommend pre-heating (aging) at low current.
05
05
Store indoors in a dry place and keep the moisture-barrier packaging intact.
If your installation or operating conditions are unusual, our engineers will review them in advance. Send a drawing or your process conditions and we will start by selecting the right material with you.
If your installation or operating conditions are unusual, our engineers will review them in advance. Send a drawing or your process conditions and we will start by selecting the right material with you.
If your installation or operating conditions are unusual, our engineers will review them in advance. Send a drawing or your process conditions and we will start by selecting the right material with you.

Advanced material supply and machining,
a global material leader
From raw material to finished part, the best solution seen from your side.
Weekdays 9:00 AM – 5:30 PM (alternate Fridays until 4:00 PM; closed weekends and public holidays)
Advanced material supply and machining,
a global material leader
From raw material to finished part, the best solution seen from your side.
Weekdays 9:00 AM – 5:30 PM (alternate Fridays until 4:00 PM; closed weekends and public holidays)

KOREA TUNGSTEN CO.,LTD
KOREA TUNGSTEN CO.,LTD
Refractory metal supply and ultra-precision machining — core materials for semiconductor, display, defense, space, medical & radiation.
INNOMT LLC
INNOMT CO.,LTD
Korea Tungsten's official overseas division
Key industries served
Customer support
© 2026 Korea Tungsten Co., Ltd. All rights reserved. 83 Bideukbawi-gil, Jori-eup, Paju-si, Gyeonggi-do 10949, Korea (364-2 Osan-ri) +82-31-975-1717
© 2026 INNOMT Co., Ltd. All rights reserved. Unit A-1710, IS Biz Tower Hangang 3, 50 Eutteum-ro, Deogyang-gu, Goyang-si, Gyeonggi-do 10543, Korea +82-2-6408-4239
Privacy Policy
Terms of Use
Cookie settings
KOREA TUNGSTEN CO.,LTD
KOREA TUNGSTEN CO.,LTD
Refractory metal supply and ultra-precision machining — core materials for semiconductor, display, defense, space, medical & radiation.
INNOMT LLC
INNOMT CO.,LTD
Korea Tungsten's official overseas division
Key industries served
Customer support
© 2026 Korea Tungsten Co., Ltd. All rights reserved. 83 Bideukbawi-gil, Jori-eup, Paju-si, Gyeonggi-do 10949, Korea (364-2 Osan-ri) +82-31-975-1717
© 2026 INNOMT Co., Ltd. All rights reserved. Unit A-1710, IS Biz Tower Hangang 3, 50 Eutteum-ro, Deogyang-gu, Goyang-si, Gyeonggi-do 10543, Korea +82-2-6408-4239
Privacy Policy
Terms of Use
Cookie settings